Introduction
In automotive manufacturing, a design change rarely affects only one component or one production process. A revised hole position, modified flange, updated material specification, or relocated assembly interface can influence stamping tools, inspection fixtures, welding fixtures, robotic programs, and downstream assembly operations.
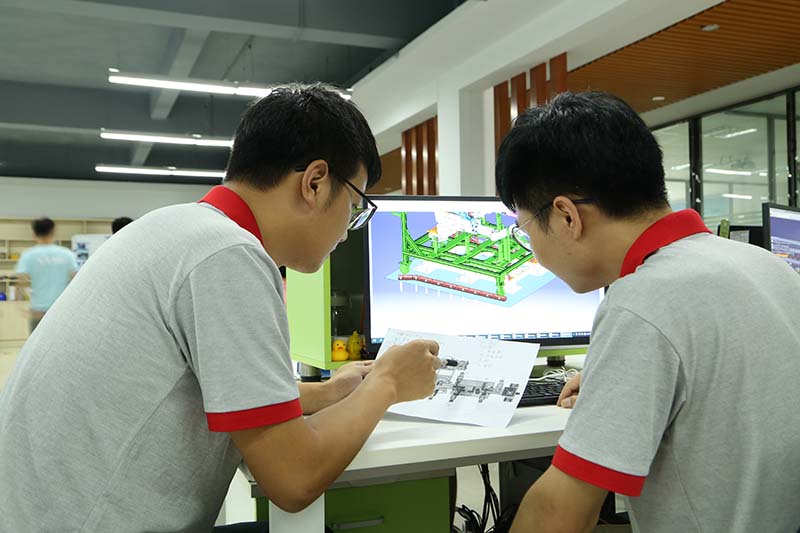
When these changes are not communicated and implemented consistently, manufacturers may encounter dimensional mismatches, repeated tooling adjustments, delayed validation, and unexpected production downtime.
CAD revision control in automotive tooling is therefore more than a document management activity. It is an engineering coordination process that ensures design intent, tooling geometry, inspection methods, and manufacturing operations remain aligned throughout product development and production.
For automotive OEMs and Tier 1 suppliers, an effective revision management process helps reduce avoidable rework and provides a clearer path from engineering approval to production readiness.
1. Why Engineering Changes Can Create Production Risks
Automotive components are manufactured through interconnected processes. A change introduced during product development may affect several downstream operations even when the visible modification appears relatively small.
Common examples include:
- A relocated mounting hole that changes the positioning strategy of an inspection fixture.
- A modified flange that requires adjustments to stamping die surfaces or forming conditions.
- A revised joining interface that affects welding fixture clamps and component accessibility.
- A changed assembly datum that influences dimensional inspection and robotic positioning.
- An updated material thickness that requires a review of forming behavior, clearances, and process parameters.
The main risk is not simply that a drawing has changed. The risk occurs when different departments or suppliers continue working with different revisions of the same component.
For example, a tooling supplier may manufacture a fixture using an earlier CAD model while the customer’s quality team has already approved a revised datum scheme. Both teams may follow their own documents correctly, yet the finished tooling may not support the same inspection requirements.
This is why revision control should be integrated into the engineering workflow rather than handled as an administrative task after a change has been released.
2. Establish One Approved Source of Engineering Data
The first step is to establish a controlled source for product and tooling information.
Before design or manufacturing begins, the project team should identify the approved CAD model, drawing revision, material specification, critical dimensions, datum references, and applicable customer requirements.
A practical document control system should distinguish between preliminary design data, data released for tooling development, and the final approved revision.
Each engineering change should also have a traceable record containing:
- The original and revised document identifiers.
- A clear description of the change.
- The reason for the change and its expected impact.
- The departments, suppliers, and tooling items affected.
- The approval status and effective date.
- The verification activities required before production release.
File naming conventions are useful, but a file name alone cannot guarantee that the correct revision is being used. Teams should also control document access, release status, revision history, and the distribution of updated files.
Where multiple suppliers participate in a project, the change notification process should confirm that each affected party has received and acknowledged the approved information.
3. Evaluate the Impact on Stamping Dies and Forming Processes
A product design revision can influence the geometry and performance of automotive stamping dies.
Changes to panel profiles, flange angles, hole locations, material thickness, or forming depth may require engineers to review the die design and the associated manufacturing process.
The impact assessment should consider more than the modified CAD surface. Engineers may need to evaluate:
- Punch and die geometry.
- Trimming and piercing positions.
- Forming clearances and material flow.
- Potential interference during tool operation.
- Part springback and dimensional stability.
- Existing machining, assembly, and tryout status.
For tooling that has already entered manufacturing, the team should determine whether the change can be implemented through localized modifications or whether a broader redesign is necessary.
The decision should be based on the actual geometry, manufacturing stage, technical risk, and customer approval requirements.
TTM Group provides automotive stamping tooling solutions for different component geometries and production requirements. Explore the automotive stamping die and tooling solutions to learn more about its tooling capabilities.
4. Update Inspection Fixtures Alongside Product Design Changes
Inspection fixtures must reflect the approved product geometry and the intended measurement strategy.
A revision affecting a locating hole, reference surface, profile, or assembly interface may change how a component is positioned and inspected. If the inspection fixture remains based on an outdated model, dimensional results may become difficult to interpret or compare with the latest product requirements.
During an engineering change review, the quality and fixture engineering teams should confirm:
- Whether the primary and secondary datum references remain valid.
- Whether locating pins, support blocks, and clamps require modification.
- Whether measurement points or checking features have changed.
- Whether the existing inspection procedure remains applicable.
- Whether fixture recertification or a new correlation study is required.
It is also important to distinguish between a change to the physical part and a change to the inspection method. These changes may have different consequences for existing measurement results and quality records.
For applications involving complex body structures, stamped components, or assemblies, TTM Group offers customized automotive inspection fixture solutions.
Coordinating fixture updates with engineering releases helps manufacturers maintain a consistent relationship between product design and dimensional verification.
5. Check Welding Fixtures and Robot Programs for Compatibility
When an automotive component changes, the welding process may also require review.
A modified flange, joining surface, hole pattern, or component interface can influence clamp positions, locator design, weld access, and assembly sequence. In automated production, the same change may affect robot approach paths, tool clearances, and the position of the workpiece relative to the welding equipment.
An effective change review should consider both mechanical tooling and control-related adjustments.
The team should verify:
- Whether the revised component can be located repeatably.
- Whether clamps and locating elements still provide suitable support.
- Whether welding access and torch clearance are maintained.
- Whether robot paths or welding positions need to be updated.
- Whether safety checks and interlocks remain valid.
- Whether trial production and dimensional validation are required.
Not every design revision requires a complete robot reprogramming exercise. The required action depends on the size and location of the change, the existing cell configuration, and the approved process definition.
TTM Group provides automated welding fixture line solutions for automotive manufacturing applications. Reviewing the fixture, robot program, and inspection requirements together can help prevent a localized design change from creating a downstream production problem.
6. Use a Structured Engineering Change Review
A structured review helps the project team identify affected tooling before modifications begin.
The review can be organized into five practical stages.
Stage 1: Identify the Change
Compare the newly released CAD model and drawings with the previously approved revision. Identify modified geometry, dimensions, material requirements, interfaces, and functional characteristics.
Stage 2: Map the Affected Manufacturing Assets
Determine which stamping dies, inspection fixtures, welding fixtures, robot programs, assembly equipment, and inspection documents may be affected.
Stage 3: Assess Technical and Commercial Impact
Estimate the required engineering work, machining or fabrication changes, procurement needs, validation activities, and potential schedule implications. Confirm responsibilities with the relevant customer and suppliers.
Stage 4: Implement and Verify the Change
Complete the approved modifications and carry out the necessary dimensional checks, tooling trials, process validation, and documentation updates.
Stage 5: Release the Updated Process
Confirm that the revised documents are approved, obsolete information is clearly controlled, and the relevant production and quality teams are working with the same revision.
This process does not eliminate every engineering risk, but it makes the consequences of design changes more visible and manageable.
7. Define Verification Requirements Before Production Release
A revised CAD model should not automatically be treated as evidence that modified tooling is ready for production.
Verification requirements should be established according to the nature of the change and its effect on product quality and process performance.
Depending on the application, verification may include dimensional inspection, fixture repeatability checks, stamping tryouts, welding trials, robot path confirmation, and first-off component evaluation.
The team should also identify the acceptance criteria before testing begins. These may include critical dimensions, datum relationships, assembly fit, weld quality, and process-specific requirements.
If a change affects several manufacturing stages, the verification plan should cover the relevant interfaces rather than validating each item in isolation.
For example, a stamped component may satisfy its dimensional requirements while still causing an assembly problem if its locating interface has changed. A fixture modification may also appear mechanically correct but require confirmation through the agreed inspection method.
Clear release criteria help the project team distinguish between a completed modification and a fully verified production solution.
8. How an Integrated Tooling Supplier Can Support Change Management
When stamping tools, inspection fixtures, welding fixtures, and automation equipment are developed by separate suppliers, engineering changes may require repeated communication and independent impact assessments.
An integrated tooling partner can help coordinate these activities by reviewing the related manufacturing requirements within a broader engineering context.
TTM Group’s capabilities cover automotive stamping dies, inspection fixtures, welding fixtures, and customized automation equipment. This range of manufacturing solutions can support coordination between product geometry, tooling design, dimensional verification, and production equipment.
Learn more about TTM Group’s automotive manufacturing solutions or explore its automated welding equipment and fixture capabilities.
For each project, the actual scope of engineering coordination should be agreed upon in advance, including document ownership, revision approval, tooling modification responsibilities, validation requirements, and production release criteria.
Conclusion
CAD revision control is an important part of managing engineering risk in automotive tooling projects. Its value comes from ensuring that every affected process responds to the same approved design information.
By establishing controlled engineering data, evaluating the impact on stamping dies, updating inspection fixtures, reviewing welding and automation requirements, and defining verification criteria before release, manufacturers can reduce avoidable rework and improve production readiness.
For automotive OEMs and Tier 1 suppliers, effective engineering change management supports more predictable tooling development and better coordination across the manufacturing process.
TTM Group provides automotive tooling and manufacturing solutions covering stamping dies, inspection fixtures, welding fixtures, and automation equipment. To discuss a project involving tooling development, engineering changes, or manufacturing integration, contact the TTM Group team through the official website.
Post time: Oct-19-2026

.png)
.png)