

Heavy-Duty Progressive Stamping Die for 3.0mm S500MC Automotive Steel Parts
Product Overview
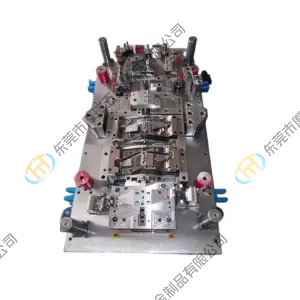
This heavy-duty automotive progressive stamping die is engineered for the continuous production of high-strength steel components using 3.0 mm S500MC hot-rolled steel coil. The tooling is designed to manufacture paired left-hand and right-hand components within a single press stroke, providing an integrated production solution for automotive sheet metal manufacturing.
Designed for operation on a 2,500-ton FAGOR stamping press, the progressive die combines a large-scale tooling structure with controlled strip feeding, precise positioning and coordinated stamping operations. Its configuration supports continuous coil-fed production while meeting the dimensional and manufacturing requirements defined for the automotive components.
With a total tooling weight of approximately 34,400 kg, this project demonstrates TTM’s engineering experience in developing large and heavy-duty progressive stamping dies for high-strength automotive steel applications.
Key Engineering Features
1. Progressive Die Design for Paired Left and Right Components
The tooling adopts a progressive stamping process in which sheet metal is continuously fed through sequential working stations.
One left-hand component and one right-hand component are produced per press stroke. This paired production arrangement supports balanced manufacturing output and reduces the need for separate production cycles for the two component orientations.
The strip layout is designed around a material width of 1,058 mm and a feed pitch of 281 mm. The layout can be optimized when necessary, provided that the total material consumption does not exceed the original requirement.
2. Processing 3.0mm High-Strength S500MC Steel
One of the main engineering considerations for this project is the forming of 3.0 mm S500MC high-strength steel.
The material is specified according to EN 10149-2, with the following mechanical properties:
- Tensile strength: 550–700 N/mm²
- Minimum yield strength: 500 N/mm²
- Minimum elongation: 14%
- Material thickness: 3.0 mm
- Thickness tolerance: ±0.2 mm
Processing high-strength steel requires careful consideration of forming forces, material behavior, dimensional stability and tool durability.
The tooling specification requires forming simulation using AutoForm, with material properties and process conditions incorporated into the engineering evaluation. Simulation results are assessed against the specified limits for failure, thinning, major strain and wrinkling.
3. Heavy-Duty Tooling Structure for a 2500T Press
The progressive die is designed for installation on a 2,500-ton FAGOR press.
Its large-scale structure is engineered to accommodate the required working forces and maintain stable operating conditions during continuous stamping production.
Key tooling dimensions and weight:
- Overall die dimensions: 4,640 × 1,978 × 1,485 mm
- Total die weight: 34,400 kg
- Upper die weight: 19,050 kg
- Tool shut height: 1,250 ± 5 mm
- Compatible press: 2,500T FAGOR
The required production force must remain within 70% of the nominal press capacity, according to the project specification.
Structural design, guiding arrangements and force-balancing elements are important considerations for maintaining tooling stability and reducing unnecessary loading during operation.
4. Precision Strip Guiding and Positioning
Stable strip movement is essential for progressive stamping, particularly when producing paired components from high-strength steel.
The tooling specification includes dedicated guiding and positioning arrangements to maintain consistent strip movement throughout the production cycle.
The pitch control system is positioned on the operator side of the strip. Fixed guiding bars are used on the pitch-control side, while the opposite guiding bars are designed with tool-free movable adjustment.
The strip must also be removable from the tooling within one minute without using additional tools.
These engineering requirements support convenient tooling operation, material handling and maintenance activities.
5. Production Stability and Tool Durability
The project is designed to meet the specified production requirements for continuous automotive manufacturing.
The main production targets include:
- Minimum production speed: 22 strokes per minute (SPM)
- Production output: One left-hand and one right-hand component per stroke
- Average annual production quantity: 52,000 left-hand and 52,000 right-hand components
- Peak annual production increase: 30%
- Required tooling durability: 7,000 left-hand and 7,000 right-hand components without interference-related maintenance
- Specified tooling service life: 9 years
The tooling design also incorporates adjustable bending elements to support geometry correction during press trials and subsequent production adjustments.
Before final acceptance, the specified welded tooling elements must be replaced with new components. Actual tooling conditions must also be scanned and compared with the approved 3D design before shipment.
Technical Specifications
| Item | Specification |
|---|---|
| Product Type | Automotive Progressive Stamping Die |
| Stamping Process | Progressive Stamping |
| Workpiece Material | S500MC |
| Material Standard | EN 10149-2 |
| Material Thickness | 3.0 mm |
| Strip Width | 1,058 mm |
| Feed Pitch | 281 mm |
| Production Output | 1 LH + 1 RH per stroke |
| Compatible Press | 2,500T FAGOR |
| Die Dimensions | 4,640 × 1,978 × 1,485 mm |
| Total Die Weight | 34,400 kg |
| Upper Die Weight | 19,050 kg |
| Shut Height | 1,250 ± 5 mm |
| Minimum Production Speed | 22 SPM |
| Design Service Life | 9 years |
Engineering and Manufacturing Considerations
For large progressive stamping dies processing high-strength steel, tooling performance depends on more than dimensional accuracy. Material utilization, forming feasibility, production stability and maintenance accessibility must all be considered during the engineering process.
For this project, the technical requirements include:
- AutoForm forming simulation and process feasibility evaluation.
- Strip layout optimization to control gross material consumption.
- Evaluation of forming force and press capacity.
- Adjustable bending elements for geometry correction.
- Dedicated guiding and positioning arrangements.
- Scanning and comparison of the completed tooling against the 3D design before shipment.
- Replacement of specified welded tooling elements before final acceptance.
These requirements establish an engineering framework for developing a stable progressive stamping process for heavy-gauge, high-strength automotive steel components.
TTM Automotive Stamping Die Manufacturing Capability
TTM Group provides customized automotive stamping die design and manufacturing services for global automotive OEMs and Tier 1 suppliers.
Our tooling portfolio includes progressive dies, transfer dies, tandem dies and other customized sheet metal forming tools for automotive body structures, reinforcements and metal components.
With engineering experience in high-strength steel applications and large-scale stamping tooling, TTM supports customers throughout tooling development, manufacturing, tryout and dimensional verification.
Explore our related solutions:
- Automotive Stamping Dies and Tools – Explore TTM’s range of automotive stamping dies and tooling solutions.
- Automotive Progressive Stamping Die for Structural Components – Learn about progressive tooling for automotive structural components.
- 5-Operation Automotive Transfer Die for Precision Sheet Metal Forming – Discover another automotive stamping tooling solution using transfer die technology.
Request a Custom Automotive Progressive Stamping Die
Looking for a reliable progressive stamping die manufacturer for high-strength steel automotive components?
TTM Group provides customized tooling solutions based on part geometry, material specifications, production volume and press capacity.
Contact our engineering and sales team to discuss your next automotive stamping die project.
Email: ttm@ttmgauge.com
Website: https://www.group-ttm.com/


.png)
.png)